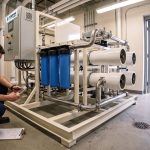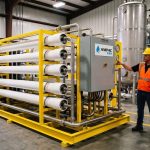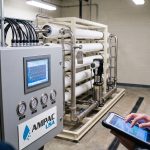
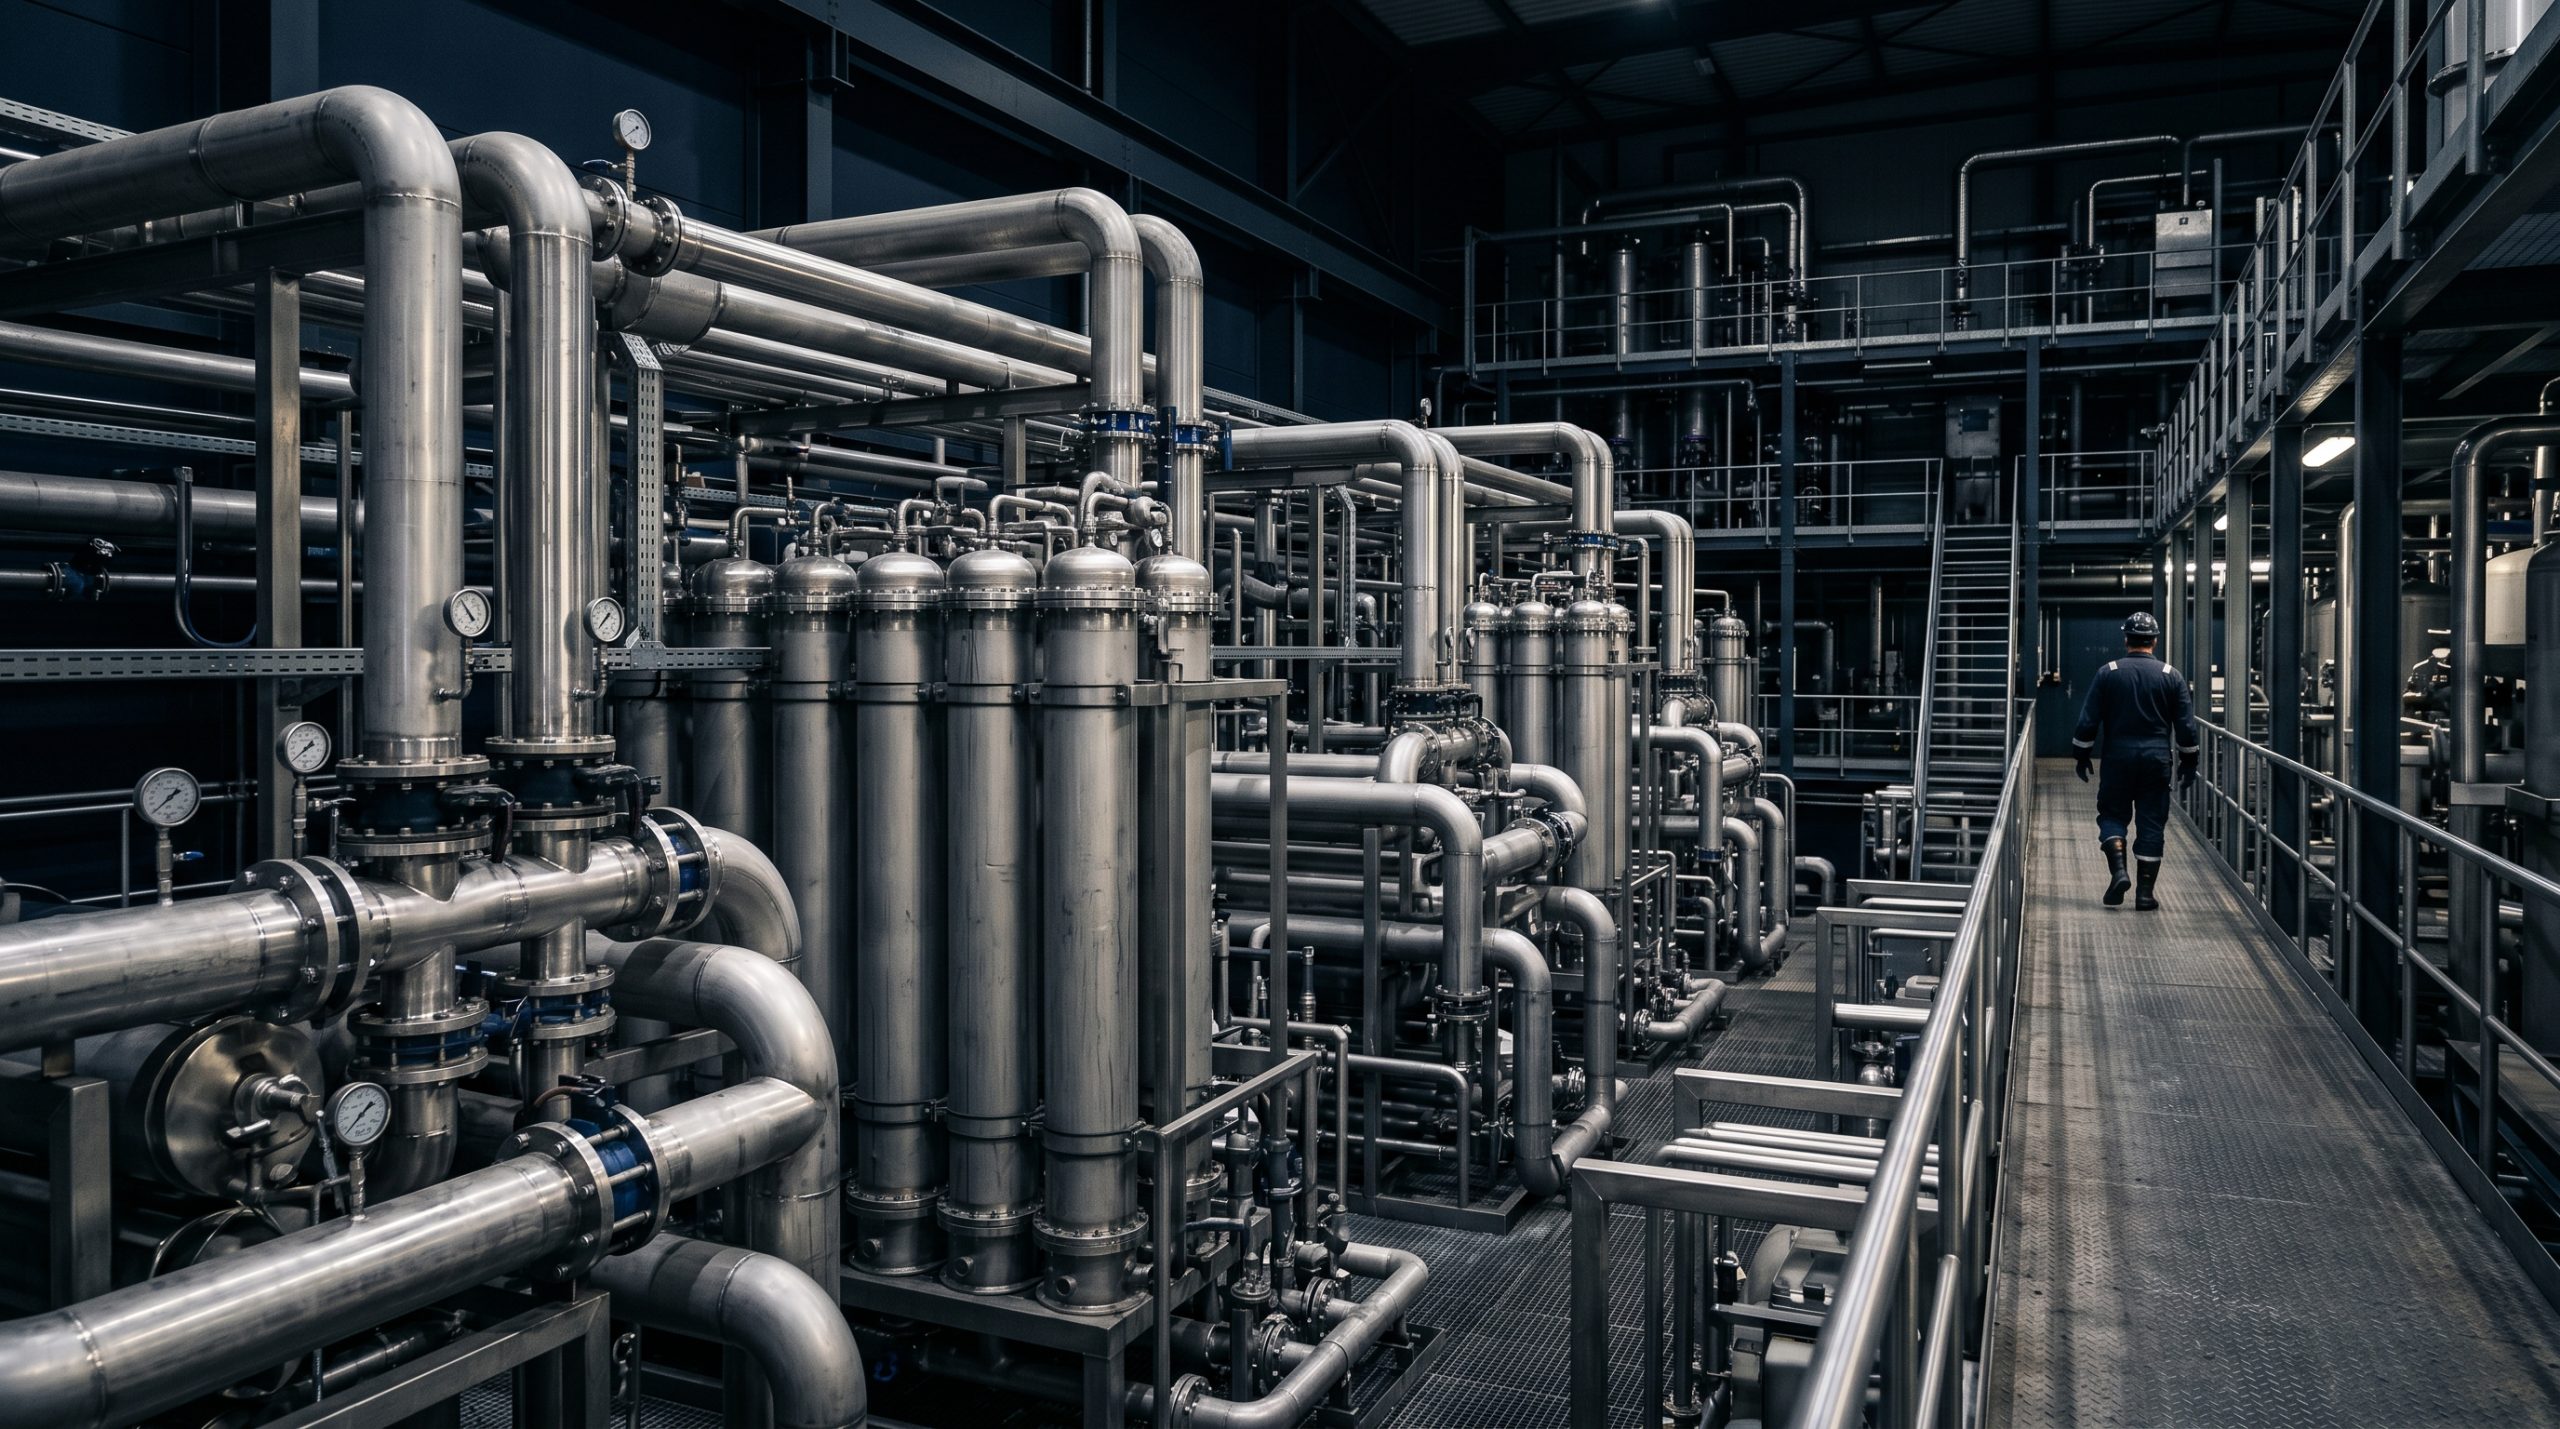

An industrial reverse osmosis system is a high-capacity water purification unit that forces pressurized feedwater through semi-permeable membranes to remove up to 99.5% of dissolved salts, heavy metals, bacteria, and organic contaminants. These systems are engineered for continuous operation at flow rates ranging from 6,000 to 100,000+ gallons per day (GPD), making them the standard solution for power plants, pharmaceutical manufacturers, food processing facilities, and military operations. Unlike residential units, industrial RO systems incorporate multi-stage pre-treatment, high-pressure pump assemblies, and automated control systems designed to handle feed water with TDS levels up to 5,000 mg/L.
Quick Summary: Industrial RO Systems at a Glance
- Flow rates: 6,000 – 100,000+ GPD (custom configurations available)
- Salt rejection: Up to 99.5% TDS removal
- Operating pressure: 150 – 600 PSI depending on feed water TDS
- Applications: Power generation, pharmaceuticals, food & dairy, military, municipal
- Key standards: NSF/ANSI 58 certified components, ISO 9001 manufacturing
- AMPAC USA experience: 35+ years engineering industrial RO systems, deployed in 40+ countries
Industrial Reverse Osmosis Systems: A Complete Technical Guide
In today’s water-stressed industrial environment, the demand for high-purity process water is non-negotiable. From microelectronics fabrication requiring ultrapure water below 0.1 µS/cm conductivity, to boiler feed water systems that must maintain TDS under 1 mg/L to prevent scale damage, industrial RO systems have become the backbone of water treatment infrastructure worldwide. According to the Global Water Intelligence Market Report, the industrial water treatment market exceeded $12 billion in 2023 and is projected to grow at 7.2% CAGR through 2028 — driven largely by increasing regulatory pressure and industrial expansion in water-scarce regions.
At AMPAC USA, founded in 1994, we have spent over 30+ years engineering, manufacturing, and deploying reverse osmosis systems across six continents. This guide provides a complete technical reference for facility engineers, plant managers, and procurement professionals evaluating industrial RO solutions.
What Is an Industrial Reverse Osmosis System?
An industrial reverse osmosis system is a large-scale water purification platform that applies hydraulic pressure — typically 150 to 600 PSI — to push source water through polyamide thin-film composite (TFC) membranes. The membrane’s pore structure, approximately 0.0001 microns, physically blocks dissolved ions, bacteria, viruses, and organics while allowing water molecules to pass through as permeate. The concentrated contaminants exit as reject (brine) at a recovery ratio typically between 50% and 85% depending on system design and feed water chemistry.
Unlike nanofiltration, which primarily targets divalent ions, RO membranes reject monovalent ions including sodium chloride — achieving TDS reductions from thousands of mg/L down to single-digit mg/L in a single pass. Compared to thermal distillation, industrial RO reduces energy consumption by up to 80%, making it the most cost-effective desalination and purification technology at scale.
Key Components of Industrial RO Systems
A well-engineered industrial reverse osmosis system rated for 6,000–100,000 GPD incorporates the following subsystems:
- Pre-Treatment Train: Multi-media filters (sand, anthracite, garnet) remove suspended solids down to 10–25 microns. Activated carbon beds adsorb chlorine and chloramines that would degrade polyamide membranes. 5-micron cartridge filters provide final protection before the high-pressure pump. Antiscalant dosing systems prevent calcium carbonate, calcium sulfate, and silica scaling on membrane surfaces.
- High-Pressure Pump Assembly: Stainless steel multistage centrifugal pumps — typically Grundfos CR or equivalent — deliver 150–600 PSI to overcome osmotic pressure and drive permeate flux through the membrane elements. Variable frequency drives (VFDs) allow flow-rate adjustment while reducing energy consumption by 20–40% compared to fixed-speed operation.
- Pressure Vessel Array and RO Membrane Elements: Industrial systems use 4-inch or 8-inch pressure vessels housing 2–7 spiral-wound RO membrane elements per vessel. Dow FILMTEC BW30-400, AXEON HF5-8040, and similar high-rejection elements are rated for 99.5% NaCl rejection. Array configurations (2:1, 3:2) balance permeate recovery and flow distribution.
- Permeate and Concentrate Manifolds: Fiberglass or stainless steel manifolds collect product water and route reject to drain or recovery systems. Energy recovery devices (pressure exchangers) on high-TDS applications can recover 40–60% of hydraulic energy from the reject stream.
- Post-Treatment: Depending on application, post-treatment may include degasification (CO₂ removal), remineralization for drinking water applications, UV disinfection at 254 nm for microbial control, or mixed-bed deionization (DI) polishing for semiconductor-grade ultrapure water.
- PLC-Based Control and SCADA: Modern industrial RO systems incorporate programmable logic controllers monitoring feed pressure, permeate conductivity, flow rates, and system recovery in real time. Remote SCADA connectivity allows centralized monitoring of multiple systems across a facility or campus.
Industrial RO System Specifications: Performance Parameters
| Parameter | Typical Range | High-Performance Target |
|---|---|---|
| Feed water TDS | 200 – 5,000 mg/L | < 2,000 mg/L for optimal recovery |
| Permeate TDS | 1 – 50 mg/L | < 10 mg/L |
| Salt rejection rate | 97 – 99.5% | 99.5% (new membranes) |
| Operating pressure | 150 – 600 PSI | 200 – 400 PSI (brackish) |
| System recovery | 50 – 85% | 75–80% (brackish water) |
| Flow rate range | 6,000 – 100,000+ GPD | Custom multi-train configurations |
| Membrane element life | 3 – 7 years | 5+ years with proper pre-treatment |
Applications: Where Industrial RO Systems Are Deployed
The versatility of water treatment technologies based on reverse osmosis makes them suitable across virtually every water-intensive industry.
Power Generation and Utilities
Power plants require ultrapure water for steam generation and turbine protection. Boiler makeup water must meet strict purity criteria — typically conductivity below 0.1 µS/cm after mixed-bed polishing — to prevent boiler tube scaling and corrosion. Similarly, chiller makeup water treated by industrial RO reduces scaling, extends equipment life, and lowers chemical treatment costs. In the energy sector, cooling tower blowdown recovery using RO can reduce freshwater intake by 30–50%.
Pharmaceutical and Life Sciences
The pharmaceutical industry operates under USP Purified Water and Water for Injection (WFI) standards requiring conductivity below 1.3 µS/cm at 25°C. AMPAC USA’s pharmaceutical-grade RO systems are designed to NSF/ANSI 58 standards with 316L stainless steel wetted surfaces, electropolished finish, and full GMP documentation packages including Factory Acceptance Testing (FAT) protocols.
Food & Beverage Processing
In the food & dairy industry, reverse osmosis concentrates whey proteins, reduces sugar content in juices, and produces high-purity process water that complies with FDA 21 CFR Part 110 food safety regulations. Industrial RO systems used in dairy processing can reduce effluent volumes by up to 70%, cutting wastewater disposal costs significantly.
Military and Remote Deployments
AMPAC USA has supplied commercial RO systems and large-scale industrial units to the United States Army, United States Navy, South Korean Navy, and Philippine Navy for expeditionary water production in remote and austere environments. Military-grade systems are containerized, ruggedized for transport by air, land, or sea, and capable of processing brackish groundwater, surface water, or seawater to potable standards in the field.
How Industrial Reverse Osmosis Works: Step-by-Step Process
- Source water intake: Feed water enters from municipal supply, groundwater well, surface water intake, or process recycle stream. Feed water TDS is measured and baseline chemistry analyzed (hardness, alkalinity, iron, silica, SDI).
- Pre-treatment: Suspended solids are removed by media filtration. Chlorine and oxidants are reduced by activated carbon or sodium bisulfite dosing. Antiscalant is injected to inhibit scale-forming mineral precipitation on membranes. SDI (Silt Density Index) is targeted below 5, ideally below 3.
- High-pressure pumping: A multistage stainless steel pump raises feed water pressure to 150–600 PSI (higher for seawater at 800–1,200 PSI). VFD control optimizes pump speed for flow demand.
- Membrane separation: Pressurized feed water enters pressure vessels and flows tangentially across RO membrane elements. Water molecules permeate through the thin-film composite membrane at flux rates of 7–14 GFD (gallons per square foot per day). Dissolved ions, bacteria, endotoxins, and organics are rejected and exit as concentrate.
- Permeate collection: Product water (permeate) is collected and routed to a storage tank or directly to point of use. Permeate conductivity is continuously monitored; any increase indicates membrane degradation or bypass.
- Post-treatment (application-specific): Pharmaceutical and semiconductor applications add mixed-bed DI polishing. Potable water applications add remineralization and disinfection. Boiler feed systems may add deaeration and oxygen scavenging.
- Concentrate management: Reject stream is routed to drain, evaporation, zero-liquid discharge (ZLD) system, or secondary use. Modern systems with energy recovery devices recapture hydraulic energy from the reject stream.
Industrial RO vs. Alternative Purification Technologies
When evaluating large-scale water purification approaches, industrial RO consistently outperforms alternatives across the key metrics of energy efficiency, rejection performance, and total cost of ownership:
- RO vs. Distillation: Compared to multi-effect distillation (MED) or multi-stage flash (MSF) evaporation, industrial RO reduces energy consumption by up to 80%. Distillation requires 10–15 kWh per cubic meter; modern RO systems operate at 3–5 kWh/m³ for brackish water.
- RO vs. Nanofiltration (NF): Unlike nanofiltration, RO membranes reject monovalent ions including sodium, chloride, and fluoride, making RO essential where full TDS reduction is required. NF is suitable for selective divalent ion removal (hardness) but not for desalination or ultrapure water production.
- RO vs. Ion Exchange: Ion exchange resin systems produce very high-purity water but require frequent chemical regeneration (acid and caustic), generating hazardous regenerant waste. Industrial RO as a pre-treatment step upstream of mixed-bed DI dramatically extends resin life — typically by a factor of 10x — reducing chemical consumption and waste disposal costs.
- RO vs. Ultrafiltration (UF): UF membranes (0.01–0.1 micron) effectively remove bacteria, viruses, and colloids but do not reduce dissolved TDS. RO is required downstream of UF when both particulate removal and dissolved solids reduction are needed.
Industrial RO System Sizing: Key Design Inputs
When your facility needs 50,000 GPD of process water with feed water TDS above 1,500 mg/L, an industrial RO system rated for 75,000 GPD feed flow (at 75% recovery) provides the correct permeate volume while maintaining sustainable flux rates on the membrane array. Proper system sizing requires the following inputs:
- Required permeate flow (GPD): Peak demand plus buffer for membrane fouling over time
- Feed water analysis: Full ion analysis (calcium, magnesium, sulfate, chloride, iron, silica), TDS, pH, alkalinity, temperature, turbidity, SDI
- Recovery target: Higher recovery reduces waste but increases concentrate TDS and scaling potential; balance with site discharge limits
- Temperature range: Membrane permeability decreases ~3% per °C reduction; cold climates require upsizing or feed water heating
- Pretreatment requirements: Determined by feed water SDI and fouling potential (biological, colloidal, scaling)
- Post-treatment requirements: Application-specific purity targets drive post-RO polishing design
AMPAC USA uses WAVE (Water Application Value Engine) modeling — the same software platform developed by DuPont Water Solutions — to optimize membrane array configurations and predict long-term performance for each installation.
AMPAC USA: Industrial RO System Credentials
Founded in 1994 and headquartered in Woods Cross, UT, AMPAC USA has accumulated over 30+ years of design, manufacturing, and deployment experience across the full spectrum of industrial water treatment. Our engineering credentials include:
- NSF/ANSI 58 certified components across our commercial and industrial product lines
- ISO 9001 quality management governing design, manufacturing, and quality control processes
- Military contract experience: US Army, US Navy, South Korean Navy, Philippine Navy — systems designed for harsh field conditions and rapid deployment
- 40+ countries served across six continents including Middle East desalination projects, Southeast Asian industrial deployments, and North American municipal installations
- UL-listed electrical components and ASME-rated pressure vessels for code compliance
- Full lifecycle support: Installation, commissioning, operator training, preventive maintenance programs, and membrane replacement services
Our industrial RO systems are built in-house at our California manufacturing facility, allowing complete quality control from component procurement through final system testing before shipment.
Frequently Asked Questions: Industrial Reverse Osmosis Systems
What is the primary function of an industrial reverse osmosis system?
An industrial reverse osmosis system is a high-capacity water purification unit designed to force pressurized feedwater through semi-permeable membranes. This process effectively removes up to 99.5% of dissolved salts, heavy metals, bacteria, and organic contaminants, producing high-purity process water for various industrial applications.
How do industrial RO systems differ from residential models?
Industrial RO systems are engineered for continuous operation and significantly higher flow rates, ranging from 6,000 to 100,000+ GPD, compared to residential units. They incorporate multi-stage pre-treatment, robust high-pressure pump assemblies, and automated control systems capable of handling feed water with TDS levels up to 5,000 mg/L.
Which industries commonly utilize industrial reverse osmosis for water purification?
Industrial RO systems are critical for sectors requiring high-purity water, including power generation, pharmaceutical manufacturing, food and beverage processing, and military operations. They are also essential for microelectronics fabrication, which demands ultrapure water below 0.1 µS/cm conductivity, and boiler feed water systems.
What level of contaminant removal can be expected from an industrial RO system?
Industrial RO systems are highly effective, capable of removing up to 99.5% of dissolved salts, heavy metals, bacteria, and organic contaminants from source water. This high rejection rate allows them to produce water suitable for sensitive applications like boiler feed, maintaining TDS under 1 mg/L.
What are the typical operating pressures and flow rates for AMPAC USA’s industrial RO systems?
AMPAC USA’s industrial RO systems are engineered for continuous operation with flow rates typically ranging from 6,000 to over 100,000 gallons per day (GPD), with custom configurations available. Operating pressures generally fall between 150 and 600 PSI, depending on the feed water’s Total Dissolved Solids (TDS) levels.
Related Articles
- Why Industrial Reverse Osmosis Treatment Is Vital for Pure Water Supply
- Industrial Reverse Osmosis Service: Expert Maintenance Tips for Maximum Efficiency
- Effective Reverse Osmosis Water Filter for Microplastics in Industrial Applications
- Boiler Feedwater Reverse Osmosis: Treatment Guide for Industrial Boilers
Conclusion
Industrial RO comes down to matching membrane count, pretreatment, and recovery rate to your actual feedwater and throughput — get that wrong and you’re either paying for capacity you don’t use or starving a process that needs more. AMPAC USA builds systems from the 6,000 GPD range up through multi-hundred-thousand GPD installations, engineered around the specs covered above rather than sold as a one-size-fits-all skid. Whether you’re running boiler makeup, chiller loops, or a pharmaceutical process line, the right design work upfront saves years of maintenance headaches later. Browse our industrial RO systems, or contact our team at info@ampac1.com or (909) 548-4900 to talk through sizing for your facility.
AMPAC USA engineers custom water purification systems for commercial, industrial, and emergency applications — from 500 GPD to multi-million GPD. Trusted by municipalities, military, and industry worldwide.