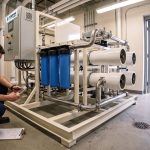


Industrial Reverse Osmosis (RO) Systems from Ampac USA deliver high-volume, high-reliability purified water for demanding environments – manufacturing, energy, food & beverage, electronics, pharmaceuticals, marine, and municipal support. Built on rugged skids with continuous-duty components, advanced PLC/HMI controls, and optimized membrane arrays, these systems reduce TDS, hardness, silica, organics, microbes, and a broad spectrum of dissolved contaminants to consistently meet EPA drinking water quality standards and tight conductivity/TDS set points while lowering total cost of ownership.
Industrial Reverse Osmosis Systems – Overview
Industrial facilities need water that is predictable, compliant, and cost-effective. Ampac USA systems are engineered for:
- Large flow rates (from thousands to hundreds of thousands of GPD) with stable permeate quality.
- High recovery via antiscalant dosing and staged membranes, lowering reject volumes.
- Operational resilience with robust pre-treatment, conservative flux rates, and 24/7 monitoring.
- Rapid serviceability using modular, skid-mounted designs and standardized spares.
Reduced scale and corrosion, improved process yields, shorter rinse cycles, lower energy in boilers/chillers, and measurable OPEX savings.
Read More: How a Water Treatment Plant RO System Works
Industrial RO System Platforms
Engineered-to-order and standard skids provide:
- Flow: configurable to production needs (e.g., 6,000-100,000+ GPD per train).
- Frames: powder-coated aluminum or stainless steel with forklift pockets and lift points.
- High-efficiency pumps: end-suction or multistage, VFD-ready for gentle ramping and energy savings.
- Membranes: 8″ spiral-wound TFC elements configured in staged arrays for fouling control and target recovery.
- Instrumentation: inlet/outlet pressure, flow, conductivity/TDS, temperature, and optional TOC.
- Controls: industrial PLC/HMI with data logging, alarm permissives, remote I/O, and auto-flush routines.
- Safety: low-pressure cutout, high-pressure relief, leak detection, pump interlocks, and NEMA-rated enclosures.
High Purity Water Systems
For electronics, pharmaceutical, biotech, laboratory environments needing low conductivity and microbial control, Ampac USA integrates:
- Pre-treatment (multimedia, carbon, softening/antiscalant, 1-5 µm filtration).
- Primary RO sized to conservative flux.
- EDI (Electrodeionization) or MB polishers to reach sub-5 µS/cm to sub-1 µS/cm targets.
- Sanitary piping, UV/UF for microbial and endotoxin control.
Read More: When Is Ultra-Pure Water Necessary?
Mobile & Solar Water Treatment
For emergency response, military, offshore, remote mining, or pipeline construction sites:
- Trailer or containerized RO plants with plug-and-play utilities.
- Solar-assist or hybrid power where grid/diesel is constrained.
- Quick deploy manifolds, onboard storage, and rugged enclosures.
- Optional pre-treatment carts (UF, media, cartridge) for turbid sources.
Water Store Equipment
Commercial RO packages tailored for bottled water plants, bulk vending, and refill stations:
- RO production skids with hygienic design.
- Ozone/UV for bottling hygiene.
- Bottle rinsers, fillers, caps, and QC controls.
Industrial RO System’s Accessories & Consumables
Maintain uptime and quality with matched components:
- Sediment cartridges (1-5 µm), bag filters, housings.
- Activated carbon, multimedia, greensand.
- Membranes (8″ elements), pressure vessels, interconnectors.
- Pumps, valves, flowmeters, pressure transmitters.
- UV systems, storage tank vent filters, level controls.
Read More: How a Water Treatment Plant RO System Works
Water Treatment Chemicals
Right-sized chemistry extends membrane life and improves recovery:
- Antiscalants/antifoulants tuned to Langelier/Stiff & Davis indices and feed ionic loads.
- pH adjustment (acid/caustic) for optimal solubility and silica management.
- Disinfectants and biocides under controlled dosing and neutralization.
Water Quality Monitoring & Control
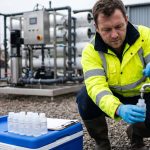
- Online TDS/conductivity with auto-divert on spec deviations.
- Permeate/reject flow balance and trending.
- DP across pre-filters and membranes to flag fouling early.
- Event/alarm logs with exportable data for audits.
- Remote access for diagnostics and optimization support.
Brackish Water Treatment Systems
Reduce TDS, hardness, iron/manganese, nitrate, and silica to meet process water or ingredient water specs. RO sizing is based on:
- Feed analysis (complete ionic profile, silica, SDI, turbidity)
- Target permeate quality (µS/cm or ppm TDS)
- Recovery (60-85% typical for brackish feeds)
- Temperature compensation and fouling risk
Water Reuse & Discharge Reduction
Rinse waters, cooling tower blowdown, or lightly contaminated streams:
- Pre-clarification/UF → RO → polish (if needed)
- Permeate returned to utilities; reject minimized via staged recovery or blending strategies
- Supports water stewardship goals and permit compliance
Ultrapure Pre-Treatment
RO is the backbone for EDI/DI when meeting sub-µS/cm specifications. Emphasis on:
- Bacteria/endotoxin control with UV/UF
- Sanitary design and hot water sanitization where required
- TOC monitoring for pharma/lab environments
Desalination & High-Salinity Feeds
For marginal or saline wells and coastal applications:
- Dual-pass RO or RO + energy recovery modules
- Antiscalant + pH programs to keep silica and sulfate scales in check
- Material selection for chloride stress corrosion resistance
Read More: Packaged Reverse Osmosis vs Traditional RO Systems
Emergency/Mobile Potable Supply
Rapid-deploy RO plants with integrated pretreatment, storage, and disinfection produce potable water during disasters, outages, or construction with operator-friendly HMIs and quick-connect utilities.
Industries we Follow:
- Food & Beverage / Dairy / Breweries: consistent ingredient water; shorter CIP/rinse cycles; improved taste and shelf life.
- Semiconductor & Electronics: low-conductivity water for rinses; particle and TOC control.
- Pharma & Biotechnology: RO + EDI + UV/UF for compliance with USP and stringent pharmaceutical quality frameworks.
- Oil & Gas / Petrochemical: boiler/chiller makeup, desalting, frac/produced water polishing (case-dependent).
- Automotive & Metal Finishing: spot-free rinsing, paint and plating line water.
- Power & Utilities: high-purity make-up prevents scaling and increases thermal efficiency.
- Municipal / Commercial Buildings: central RO for campuses, hospitals, resorts.
- Aerospace & Fastener Manufacturing: precise rinse quality for surface prep and finishing.
- Marine / Offshore / Seaports: containerized RO for bunkering and onboard processes.
- Agriculture & Hydroponics: nutrient stability via consistent feedwater.
Applications
- Boiler & Chiller Makeup: lower silica, alkalinity, and hardness for higher cycles of concentration and energy savings
- Ingredient & Process Water: stable taste/quality, reduced variability, better product yields
- Rinse & CIP: low-TDS water reduces spotting and detergent demand
- Water Reuse: reclaim rinse or blowdown streams to cut freshwater intake and discharge fees
- Pretreatment for EDI/DI: steady low-TDS feed to protect downstream polishers
Conclusion
Ampac USA is a specialist manufacturer of industrial RO Systems and commercial RO systems, desalination plants, and high-purity water solutions. The company’s philosophy blends application-specific engineering with serviceable designs that shorten downtime and extend asset life. From single-train skids to containerized and mobile solutions, Ampac USA supports global clients with engineering, commissioning, training, parts, and after-sales service.
Frequently Asked Questions
What contaminants do Ampac USA industrial RO systems remove?
Ampac USA industrial RO systems are engineered to significantly reduce a broad spectrum of dissolved contaminants. These include Total Dissolved Solids (TDS), hardness minerals, silica, organics, and microbes. The systems consistently purify water to meet EPA drinking water quality standards and tight conductivity/TDS set points.
Which industries commonly use Ampac USA’s industrial reverse osmosis systems?
Ampac USA’s industrial RO systems serve a wide range of demanding sectors requiring high-volume purified water. Key industries include manufacturing, energy, food & beverage, electronics, pharmaceuticals, marine applications, and municipal water support. Our systems are designed for critical processes in these environments.
How do Ampac USA industrial RO systems achieve high water recovery rates?
Ampac USA industrial RO systems achieve high water recovery through optimized design features like antiscalant dosing and staged membrane arrays. This approach minimizes reject volumes while maximizing the production of purified water. High recovery contributes to lower operational costs and reduced water waste.
What advanced control and monitoring features are included in Ampac USA industrial RO systems?
Ampac USA industrial RO systems feature advanced industrial PLC/HMI controls for precise operation and monitoring. These controls include data logging, alarm permissives, remote I/O capabilities, and automated auto-flush routines. Comprehensive instrumentation monitors inlet/outlet pressure, flow, conductivity/TDS, and temperature for continuous performance oversight.
How do Ampac USA systems provide ultra-pure water for sensitive applications like electronics or pharmaceuticals?
For ultra-pure water needs in electronics, pharmaceuticals, and biotech, Ampac USA integrates multi-stage purification. This includes robust pre-treatment, primary RO sized to conservative flux, and post-treatment with Electrodeionization (EDI) or MB polishers. This combination achieves extremely low conductivity targets, typically sub-5 µS/cm down to sub-1 µS/cm.
Related Articles
- Industrial RO System Components
- Industrial RO Treatment
- Ultra-Pure Water Industries
- High Purity Water Systems
Conclusion
AMPAC USA’s industrial RO lineup covers a lot of ground — high purity systems, mobile and solar platforms, brackish water treatment, and emergency potable supply units — because industrial water problems rarely fit into one box. What ties all of it together is the same engineering approach: accessories, water treatment chemicals, and quality monitoring built to work with the core RO platform rather than bolted on afterward. If you’re not sure which platform matches your application, the overview above is a good place to start narrowing it down. Contact our team at info@ampac1.com or (909) 548-4900 to talk through the right industrial RO system for your operation.
AMPAC USA engineers custom water purification systems for commercial, industrial, and emergency applications — from 500 GPD to multi-million GPD. Trusted by municipalities, military, and industry worldwide.